


World´s Largest Auto Parts Supplier Relies on Kennametal Extrude Hone for Surface Finishing
09/06/2014 Kennametal UK Ltd
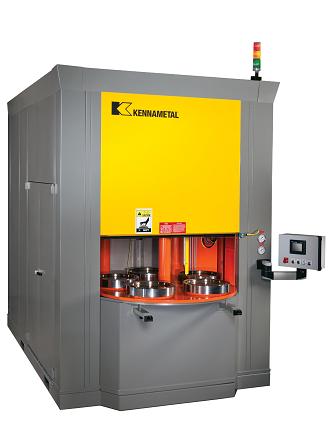
Proprietary thermal energy technology key to improved qualityNew P400 TEM machine from Kennametal Extrude Hone.Manufacturers and quality professionals in such industries as automotive, aerospace, energy, medical, and others requiring high-precision components know that removing particle left at intersected holes and ensuring no micro contamination is a quality challenge that cannot be overlooked. Customized complex valves, gears, pinions, and thousands of components can be machined in seconds but can take minutes to get finish completely. Production bottlenecks, increased costs, and longer time to market are among the results.
Kennametal Extrude Hone is a global leaded dedicated to providing Precision Surface Solutions for component of uncompromising quality. Proprietary technologies such as TEM (thermal energy machining) are solving increasingly complex finishing challenges faced by manufacturers around the world.
Delphi-TVS is a joint venture between Delphi Corp. (Troy, Michigan USA) and T.V. Sundaram Iyengar & Sons (Kancheepuram, India). Delphi is the largest automotive supplier in the world and Delphi-TVS is the largest automotive systems manufacturer in India.
"Being a global company, we have a great responsibility to maintain world-class quality standards in our products," says T.N. Umasankar, head of the Delphi-TVS manufacturing engineering department. "We manufacture diesel fuel injection parts - high-volume components. The main issue is burr removal on cross-sectional holes from previous machining operations."
Delphi-TVS faced many issues: High component volumes approaching a million a year made hand-deburring unaffordable and the high-precision nature of diesel fuel injectors made TEM solution a necessity.
After much investigation, the company chose Kennametal Extrude Hone's TEM (thermal energy method) solution. A pressurized mixture of a combustible gas and oxygen is injected at 5 to 10 atmospheres of pressure into a containment chamber sized both by the amount of material to be removed and the volume of parts in the chamber. An ignition system ignites the gas mixture, releasing heat energy from the oxidation of fuel in a 20-millisecond, high-speed energy wave. With their raised surface areas and thin cross-section features, even internal burrs and flashings burn away instantly. Because the gas mixture engulfs the entire workpiece, all internal and external surfaces are exposed to the rapid oxidation. Internal cross-drilled holes and intersecting edges that are difficult or impossible to reach are instantly processed.
"There have been hundreds of installations and continued refinement of our TEM equipment and process," says Bruno Boutantin, global marketing manager at Kennametal Extrude Hone. "One factor remains constant: TEM is a rapid, low-cost, high-production process that can process a million or more parts per year by a single machine."
"The TEM process is particularly appropriate for high-volume applications where conventional deburring departments struggle to keep pace," Umasankar agrees. "lt instantaneously cleanup a large number of intersecting holes, threads and hard-to-reach areas in a flash, literally in 20 milliseconds. Its ability to fire multiple components at the same time increases its capacity and cost-effectiveness enormously. Any other process, including high-pressure water jet, will not provide this value."
Combining vast experience gathered over more than five decades with worldwide application knowhow, Kennametal Extrude Hone offers proven solutions to many companies working in most demanding environments. Technical Centers and Centers of Excellence ensure close customer association in all critical steps -۠from the early design phases by producing small batches of components for prototyping through supporting the ramping stage in our contract shops prior to the final delivery of state-of-the-art equipment.
In India, Kennametal Extrude Hone is an integral part of Kennametal India Ltd. Situated in Bangalore, the Kennametal Extrude Hone Technical Center is well-equipped to support every customer need.
For more information, please contact:
Anna MASON
Kennametal U.K. Ltd.
Pensnett Trading Estate
Kingswinford
West Midlands
DY6 7NP
Tel: +44 1384 408060
Fax: +44 1384 4080 15
Email: anna.mason@kennametal.com
Web: www.kennametal.com
 Print this article
Process and Control Today are not responsible for the content of submitted or externally produced articles and images. Click here to email us about any errors or omissions contained within this article.